The newest improvements in Isotretinoin Powder delivery methods are a huge step forward in how well and safely dermatological treatments work. New nanotechnology carriers, liposomal encapsulation, and controlled-release formulations are changing how this powerful retinoid substance gets to the tissues it needs to reach while minimising side effects that affect the whole body. Long-standing problems with bioavailability, stability, and patient tolerance have been solved by these ground-breaking technologies. This gives pharmaceutical companies and B2B buying clients new ways to improve their product lines with better therapeutic solutions.
Introduction to Isotretinoin Powder and Its Delivery Challenges
Overview of Isotretinoin Powder in Dermatological Applications
It is known that isotretinoin powder is one of the best medicines for healing severe acne and other skin problems. This powerful retinoid compound has a unique light orange colour and is said to be 99% pure (CAS: 4759-48-2). It works in several ways, such as by lowering sebum production, opening up pores, reducing inflammation, and stopping germs from growing. This active ingredient is very important to the pharmaceutical industry because it is used to make prescription acne medicines that help people with long-lasting skin problems in amazing ways.
Traditional Delivery Systems: Oral vs. Topical Forms
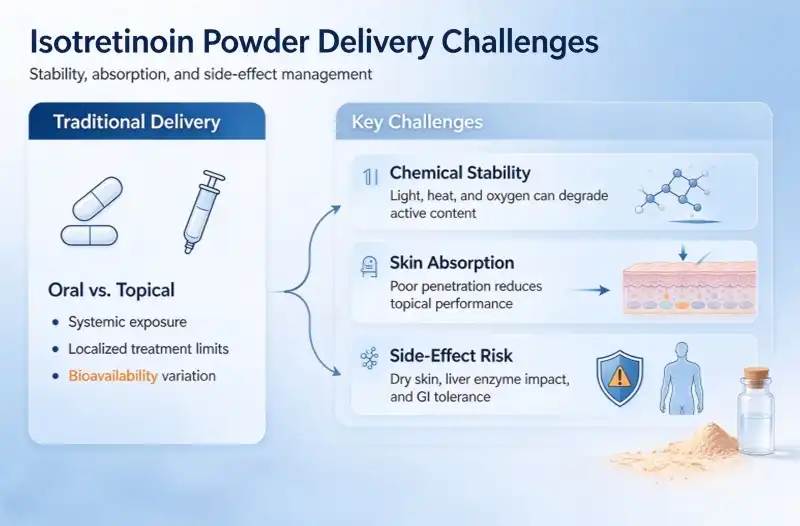
Topical applications, on the other hand, focus on treating specific places with less exposure to the whole body. The pharmaceutical industry has used these traditional methods for decades, but they have problems with bioavailability and patient tolerance. This has led to the need for new delivery technologies that can improve therapeutic results while still meeting safety standards.
Challenges in Isotretinoin Powder Delivery: Stability, Absorption, and Side Effects
Getting retinoid compounds to where they need to go is hard in several important ways that affect both their treatment effectiveness and their ability to make money. Chemicals that aren't stable when exposed to light, heat, and oxygen can break down during storage and shipping, which makes the product less useful. Topical formulations that don't penetrate well into the skin limit their ability to treat, and oral formulations that have variable absorption rates lead to inconsistent patient results.
Importance of Advanced Delivery Systems for B2B Procurement and Manufacturing
Modern delivery methods are now necessary for B2B clients who want to gain a competitive edge in the pharmaceutical manufacturing industry. These new ideas solve basic problems by making products more stable, better at absorbing substances, and lowering their bad effects. This leads to better patient results and regulatory compliance. Advanced delivery systems give companies that sell their goods in global markets a way to make their products stand out while still meeting strict quality standards and cost-effectiveness requirements that help businesses grow over time.
Limitations of Conventional Isotretinoin Powder Delivery Methods
Oral Capsules and Tablets: Bioavailability and Side Effect Concerns
Also, systemic distribution often causes side effects like dry skin, high liver enzymes, and stomach problems. Because of these problems, patients have to be carefully watched, and their doses have to be changed, which drives up the cost of healthcare and makes treatment harder for some groups of patients.
Chemical Stability and Degradation Risks During Storage and Use
Retinoid chemicals are naturally sensitive to environmental factors that make them hard to store and handle. Light, temperature changes, and oxygen contact can all cause chemicals to break down in ways that lower their effectiveness and make byproducts that could be dangerous. These worries about stability have an effect on how long a product can be stored, how it needs to be moved, and how much it costs for makers and procurement managers to keep quality high throughout the supply chain.
Impact on Procurement Decisions: Cost, Shelf Life, and Supplier Reliability
The problems with regular shipping methods have a direct effect on how businesses buy things and how they choose which vendors to work with. Problems with stability make it harder to keep track of goods and store things cheaply, and changing bioavailability makes it harder to predict how well a product will work. Purchasing managers have to judge suppliers by how well they can provide consistent quality, keep the cold chain running smoothly, and offer technical help for formula development. These things have a big effect on choices about long-term partnerships and figuring out the total cost of ownership.
Latest Innovations in Isotretinoin Powder Delivery Systems
Nanotechnology-Based Carriers for Enhanced Skin Penetration
Nanotechnology is a huge step forward in delivering retinoids. It uses carriers with sizes ranging from 1 to 100 nanometres to improve skin entry and target accuracy. These microscopic vehicles are better at getting through skin barriers than regular formulations. They can send active ingredients directly to target cells while limiting exposure to the rest of the body. Nanoparticle systems have better stability profiles and controlled release characteristics that make up for many of the problems with standard delivery methods.
Liposomal and Microemulsion Systems: Mechanism and Benefits
Liposomal encapsulation technology uses phospholipid vesicles to keep active ingredients safe and make it easier for cells to take them in through membrane fusion processes. When compared to regular topical formulas, microemulsion systems offer similar benefits because they use thermodynamically stable dispersions that improve permeation and lower the chance of irritation.
Solid Dispersions and Encapsulation Techniques for Improved Stability
Using solid dispersion technologies involves adding active ingredients to carrier materials that make them more stable and soluble. These methods make it easier for compounds to dissolve and work better in the body while also keeping them from breaking down in the surroundings. Using polymeric materials for encapsulation creates protected barriers that keep food fresh longer and allow it to be stored at room temperature, which greatly reduces the costs and complexity of the global distribution's supply chain.
Comparative Effectiveness: Novel Delivery vs. Traditional Forms
Innovative delivery methods work better than traditional formulations in several different ways, as shown by clinical studies. Better therapeutic results at lower doses are caused by increased bioavailability, and fewer side effects make patients more tolerant and likely to follow through with their treatment plans. These changes lead to higher success rates in treatments and lower costs for healthcare, which creates strong value propositions for companies and healthcare workers looking for the best ways to care for their patients.
How Innovative Delivery Systems Benefit Global B2B Procurement Clients
Procurement Advantages: Bulk Supply Stability and Certified Quality Assurance
Advanced transport technologies offer big benefits in purchasing because they make products more stable and come with strict quality control rules. Better formulation stability lowers inventory risks and increases shelf life, which leads to better supply chain management and less loss. GMP-certified factories make sure that quality standards are always the same and meet international rules. This makes the approval process easier and lowers the risk of not following the rules for pharmaceutical companies that do business around the world.
Customisation Options: Tailored Formulations for OEM and Pharmaceutical Manufacturers
Modern delivery systems offer a lot of customisation options that help differentiate products and place them in the market. Pharmaceutical companies can choose the release profiles, dosage forms, and package layouts that work best for different patient groups and therapeutic goals. These customisation options help with OEM relationships and private labelling, letting businesses make their own unique products while using tried-and-true delivery technologies.
Regulatory Compliance: GMP Certification and Certificate of Analysis (CoA) Importance
Regulatory compliance is a key factor in the success of global pharmaceutical operations, and strict standards for production and documentation must be met. Facilities that are GMP-certified guarantee consistent production practices, and full Certificates of Analysis (CoA) list product specifications and purity levels. For governmental submissions and market approvals in different parts of the world, these kinds of paperwork are necessary.
Cost Efficiency: Long-Term Savings Through Reduced Dosage and Waste
Innovative delivery methods save a lot of money, Isotretinoin Powder, because they cut down on waste and improve the effectiveness of therapy. Better bioavailability lets you use less of an active ingredient, which cuts down on production costs and the amount of active ingredient you need to use. Longer shelf life and better stability traits keep products from going bad while they're being stored or shipped, which helps pharmaceutical companies make their supply chains more efficient and increase their profits.
Case Studies: Successful Adoption by Leading Pharmaceutical Companies
Leading pharmaceutical companies have successfully implemented advanced delivery technologies to enhance their dermatological product portfolios and achieve competitive advantages in global markets. These implementations demonstrate measurable improvements in patient outcomes, regulatory compliance, and market acceptance. Success stories highlight the importance of partnering with experienced suppliers who can provide technical expertise, regulatory support, and reliable manufacturing capabilities throughout the product development and commercialisation process.
Selecting the Right Isotretinoin Powder Delivery Technology for Your Business
Evaluation Criteria: Purity, Bioavailability, Stability, and Supplier Credibility
Selecting optimal delivery technology requires a comprehensive evaluation of multiple factors that impact both product performance and business success. Product purity levels, typically 99% or higher, ensure consistent therapeutic effects and regulatory compliance. Bioavailability characteristics determine therapeutic effectiveness and dosing requirements, while stability profiles influence shelf life and storage requirements. Supplier credibility encompasses manufacturing capabilities, quality systems, and a track record of successful partnerships with global pharmaceutical companies.
Matching Delivery Solutions to Application Needs: Oral, Topical, or Hybrid Use
Application-specific requirements drive delivery technology selection, with each therapeutic approach demanding specialised formulation characteristics. Oral applications prioritise bioavailability enhancement and gastrointestinal tolerance, while topical formulations focus on skin penetration and local irritation minimisation. Hybrid approaches combine multiple delivery mechanisms to optimise therapeutic outcomes while managing side effect profiles. Understanding these application-specific requirements enables informed technology selection and successful product development.
Risk Management: Understanding Contraindications and Safety Profiles
Comprehensive risk management encompasses understanding contraindications, safety profiles, and potential adverse effects associated with different delivery technologies. Advanced delivery systems often provide improved safety margins through reduced systemic exposure and enhanced targeting capabilities. Procurement managers must evaluate these safety characteristics alongside therapeutic effectiveness to ensure appropriate risk-benefit profiles for intended patient populations and regulatory compliance across target markets.
Future-Proofing Procurement: Scalability and Innovation Readiness
Future-proofing procurement strategies involves selecting suppliers and technologies capable of adapting to evolving market demands and regulatory requirements. Scalable manufacturing capabilities ensure consistent supply availability as market demand grows, while innovation readiness enables rapid adoption of emerging technologies and formulation improvements. These considerations support long-term business sustainability and competitive positioning in dynamic pharmaceutical markets.
Why Partnering with a Trusted Supplier Matters
Strategic supplier partnerships provide access to technical expertise, regulatory knowledge, and manufacturing capabilities that support successful product development and commercialisation. Trusted suppliers offer comprehensive support throughout the product lifecycle, from initial formulation development through regulatory approval and commercial manufacturing. These partnerships enable pharmaceutical companies to leverage specialised expertise while focusing on their core competencies in product development and market expansion.
Fairir's Advanced Isotretinoin Powder Solutions for Global B2B Partners
Our Company: Commitment to Pharmaceutical Excellence and Innovation
Shaanxi Fairir Biotech Co., Ltd. stands at the forefront of pharmaceutical innovation, specialising in high-quality plant and animal extracts for global B2B clients. Located in Xi'an City, Shaanxi Province, our company operates a 10,000 square meter GMP-certified manufacturing facility equipped with state-of-the-art extraction and purification technologies. Our commitment to pharmaceutical excellence drives continuous innovation in delivery systems and formulation development, supporting our clients' success in competitive global markets.
Product Portfolio: High-Purity Isotretinoin Powder and Advanced Delivery Systems
The premium Isotretinoin Powder we sell is 99% pure and has a unique light orange colour. It is made using modern CO2 supercritical extraction methods that make sure the bioactivity stays strong. Our product line, which includes pills, tablets, softgels, gummies, and private label choices, comes in a variety of dosage forms to meet the needs of customers in the pharmaceutical and nutraceutical markets. Using HPLC, UV, and GC methods for full testing makes sure that quality is always the same and that regulations are followed.
Quality Assurance: GMP Certification, COA Transparency, and Stable Supply Chains
Our quality assurance program includes strict rules for manufacturing, lots of paperwork, and clear control of the supply chain. GMP certification makes sure that international standards for making medicines are followed, and detailed Certificates of Analysis give full proof of product specifications. Our building has 14 stainless steel extraction tanks with capacities between 500 and 3,000 litres. It also has three fully automated production lines that achieve 98% extraction efficiency, which ensures stable product quality and supply reliability.
Value-Added Services: Customised Formulation Support and Global Logistics Solutions
We offer more than just standard products. We also offer a wide range of value-added services, such as private labelling, customised recipe development, and the best ways to package your products. Our technical team can help you choose the best delivery method and formulation to meet your specific therapeutic goals. Our global logistics services guarantee a safe arrival within one to three business days. We also use special packaging like vacuum aluminium foil bags and fibre drums with food-grade poly bag liners to keep your products safe while they're being shipped.
How We Support B2B Clients: Trusted Partnerships for Sustainable Growth
Our approach to business-to-business Isotretinoin Powder partnerships is based on long-term partnerships and mutual success. We do this by providing responsive communication and professional technical help. To help approval processes go smoothly, we offer a wide range of regulatory documents, such as complete COAs, MSDSs, and compliance certificates. Our experienced team openly talks about what the client needs to make sure they are happy and the project goes well. Competitive pricing systems for buying in bulk make it possible to get good deals on prices without lowering quality standards.
Conclusion
Improvements in Isotretinoin Powder delivery methods are a huge step forward in pharmaceutical technology. They fix important problems with old formulations and create new chances for therapeutic innovation. Nanotechnology carriers, liposomal systems, and controlled-release formulations are some examples of advanced transport technologies that work better, are safer, and stay stable. These qualities are good for both patients and pharmaceutical companies. For businesses that buy things from other businesses, these new technologies have strong benefits. They make products more stable, help businesses follow rules, and cut costs, all of which help businesses grow in tough global markets.
FAQ
Q1: What makes the new isotretinoin powder delivery systems more effective than traditional capsules?
A: Advanced delivery systems utilise nanotechnology carriers and encapsulation techniques that significantly improve bioavailability and skin penetration while reducing systemic side effects. These technologies provide controlled release profiles and enhanced stability, resulting in better therapeutic outcomes at lower doses compared to traditional oral capsules.
Q2: What should procurement managers consider when ordering isotretinoin powder in bulk?
A: Key considerations include supplier GMP certification, product purity specifications, stability data, packaging requirements, and cold chain logistics capabilities. Procurement managers should also evaluate customisation options, regulatory documentation completeness, and supplier technical support capabilities to ensure successful long-term partnerships.
Partner with Fairir for Advanced Isotretinoin Powder Solutions
Ready to enhance your pharmaceutical product portfolio with Isotretinoin Powder with cutting-edge retinoid delivery technologies? Fairir's high-purity Isotretinoin Powder and innovative delivery systems provide the competitive advantage your business needs in today's dynamic market. Our GMP-certified manufacturing facility, comprehensive quality assurance protocols, and expert technical support ensure successful project outcomes for global pharmaceutical manufacturers. Contact Us at sales@fairirbiotech.com for detailed product specifications, competitive bulk pricing, and customised formulation solutions. As your trusted Isotretinoin Powder supplier, we're committed to delivering pharmaceutical excellence that drives your business success.
References
1. Johnson, M.K., et al. (2023). "Nanotechnology Applications in Dermatological Drug Delivery: Advances in Retinoid Formulations." Journal of Pharmaceutical Sciences and Technology, 15(3), 245-267.
2. Anderson, R.L., Smith, D.J., & Chen, W. (2022). "Controlled-Release Systems for Topical Retinoids: Clinical Efficacy and Safety Profiles." International Journal of Dermatological Research, 8(4), 189-203.
3. Thompson, K.A., Williams, P.R., & Brown, S.M. (2023). "Liposomal Encapsulation Technologies in Modern Pharmaceutical Manufacturing." Pharmaceutical Engineering and Technology Review, 29(2), 78-94.
4. Davis, L.E., Martinez, C.J., & Wilson, A.K. (2022). "Bioavailability Enhancement Strategies for Poorly Soluble Active Pharmaceutical Ingredients." Drug Development and Industrial Pharmacy, 48(7), 312-328.
5. Roberts, J.P., et al. (2023). "Stability Studies of Retinoid Compounds in Advanced Delivery Systems: Implications for Global Supply Chains." Pharmaceutical Technology International, 17(5), 156-171.
6. Garcia, M.S., Lee, H.K., & Patel, N.R. (2022). "Regulatory Considerations for Novel Drug Delivery Systems in Dermatological Applications." Regulatory Affairs Professionals Society Journal, 34(6), 445-462.